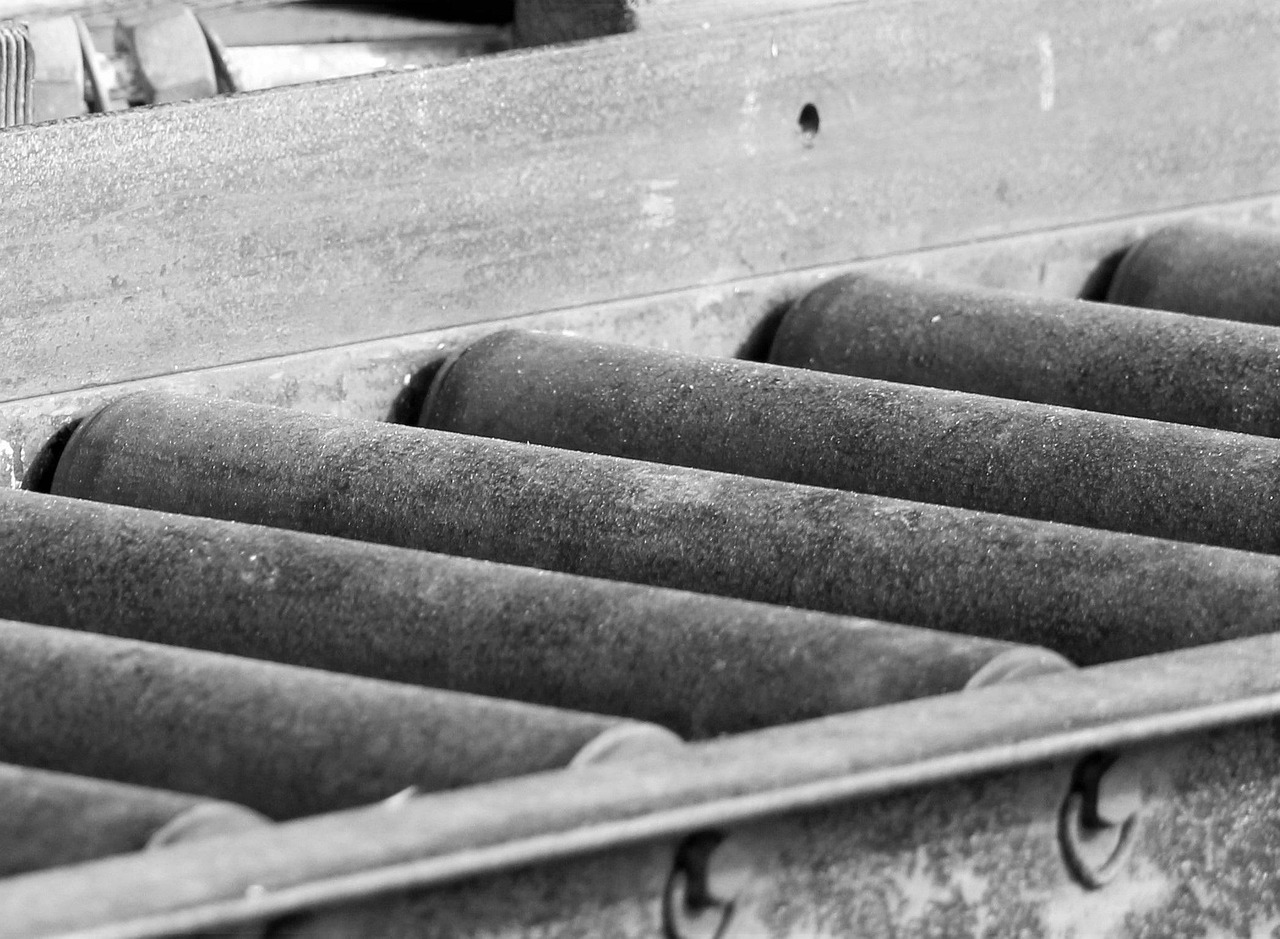
Heavy duty roller conveyor systems are an indispensable part of manufacturing and distribution environments. Designed to handle large volumes and weights, these systems are integral to the efficiency and productivity of warehouses, factories, and distribution centers worldwide. Their ability to facilitate the smooth and fast movement of bulk goods makes them a vital component in logistics operations. This guide will explore the various aspects of heavy duty roller conveyor systems, offering insights into their functionality, types, and benefits. Additionally, it will provide key considerations for selecting the right system to meet specific operational needs.
Understanding Heavy Duty Roller Conveyor Systems
Heavy duty roller conveyor systems are built for robust industrial applications. They are engineered to carry heavy loads over long distances, making them ideal for industries like automotive, mining, and manufacturing. These systems use rollers”?typically made of steel or other durable materials”?to transport items along a set path or into a processing area.
Key Features
- High load capacity: Capable of handling weights ranging from hundreds to thousands of pounds.
- Durability: Constructed from materials like stainless steel for long-lasting performance.
- Flexible configurations: Customizable to fit specific operational layouts and processes.
- Low maintenance: Designed to minimize wear and tear, reducing downtime and maintenance costs.
For further insights on these systems, discover expert strategies here.
Types of Roller Conveyor Systems
There are several types of heavy duty roller conveyor systems, each suited to different industrial needs:
- Gravity Roller Conveyors: Utilize the force of gravity to move items along the conveyor. Ideal for applications where the movement does not require powered assistance.
- Powered Roller Conveyors: Use motors to drive the rollers, providing controlled movement of goods. Suitable for process lines requiring precise handling.
- Chain-Driven Roller Conveyors: Designed for heavy-duty loading, using chains to propel the rollers. Perfect for moving pallets and large containers.
- Belt-Driven Roller Conveyors: Use belts to drive the rollers, offering smooth and quiet operation. Best for transporting smaller items or irregularly shaped products.
To explore advanced guides and tips on selecting the right type, learn about our tailored solutions.
Benefits of Implementing Heavy Duty Roller Conveyor Systems
Integrating these systems into your operations can bring numerous advantages:
- Increased Efficiency: Streamline the movement of materials, reducing manual handling and speeding up processes.
- Improved Safety: Minimize the risk of injury by automating the transport of heavy goods.
- Cost Savings: Reduce labor costs and potential damage to products through efficient handling.
- Scalability: Easily expandable to accommodate growing production needs.
For more information, find out more about this approach.
Considerations for Choosing the Right System
Selecting the appropriate heavy duty roller conveyor system requires careful consideration of several factors:
- Load Capacity: Determine the maximum weight the system needs to handle.
- Environment: Consider environmental conditions, such as temperature and humidity, which may affect system performance.
- Space Constraints: Assess available space to ensure the system fits seamlessly into existing workflows.
- Budget: Balance cost with performance, ensuring the system provides value over its lifespan.
To explore more on this topic, explore advanced guides and tips.
In conclusion, heavy duty roller conveyor systems are a critical component in modern industrial logistics. They provide the necessary infrastructure to efficiently move heavy loads, streamline operations, and support growing production demands. By understanding their features, types, and benefits, and considering key factors in selection, businesses can ensure optimal integration into their operations.
